

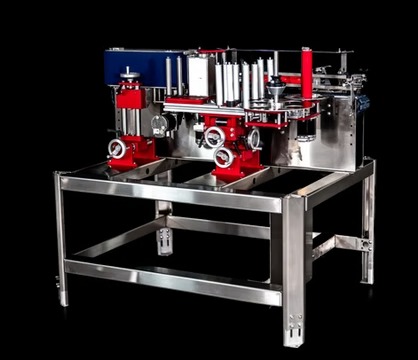
Smooth integration in lines
Every plant wants a best case conveyor machine that fits like a glove. The goal is to cut bottlenecks, not force fit parts. Start by mapping flux from intake to pack out. Look at height, belt type, drive method, and space around corners. A clear path helps operators breathe, reduce misfeeds, and trim best case conveyor machine wear on rollers. Subtle shifts in curtain walls or guardrails can shave seconds from cycles. When vendors talk efficiency, measure in real use, not spec sheets. The result is predictable motion, less jam, and a gentle, practical flow that keeps lines productive all shift long.
Materials and handling realities
Choosing a means matching the work. Heavy items need robust frames, lifted idlers, and fail‑safe stops. Delicate goods demand soft start, gentle belt tension, and precise speed control. The right system reduces product damage, lowers scrap, and simplifies maintenance. In practice, engineers custom conveyor engineering solutions assess weight, compression, and finish. Then they tailor belt materials, sprockets, and drive trains to the task, not just the price. Real life tests reveal true capacity and uncover tiny tweaks that save weeks of downtime later on.
Customization that pays off later
The best path to durable gains comes through custom conveyor engineering solutions that reflect site quirks. Narrow aisles, odd angles, overhead obstructions—these demand clever routing and safe, accessible controls. A focused plan yields a machine that resists wear and ages gracefully. Pro tips include modular subassemblies, common spare parts, and standardized mounting patterns so upgrades don’t derail production. In practice, the team previews every swap and change, so downtime stays minimal and predictability climbs as schedules tighten.
- Modular frames enable rapid reconfiguration for different SKUs
- Smart sensors catch misfeeds before they stop the line
- Standardized interfaces ease future upgrades
Practical design cues and UX
Operators win when the layout favors quick checks, fast repairs, and clear signals. A well done best case conveyor machine uses tactile controls, bright indicators, and intuitive fault codes. It also respects ergonomics: reachable pull points, low force latches, and easy belt changes. Maintenance staff benefit from clean routing paths, accessible bearings, and simple lubrication points. The end result is a line that feels human, not harsh, with fewer last‑mile hiccups that slow every shift and spike morale in a positive way.
Safety and reliability first
Safety isn’t a bolt on afterthought. The best case conveyor machine rigorously follows risk assessments and isolation protocols. Guarding is choreographed to keep hands clear without trapping operators in the action. Braking and emergency stops must be responsive, and conveyors should tolerate minor hiccups without cascading faults. A design that anticipates edge cases—like misaligned pallets or jams—saves time, reduces injury risk, and keeps QA honest about what ships out the door. Reliability grows when maintenance windows become routine, not rushed fixes.
Conclusion
Huge gains come from visibility: real time data, not vague impressions. The best case conveyor machine integrates simple dashboards that show throughput, cycle times, and alarm history. Operators spot wear trends, schedule preventive care, and plan line resets around bottlenecks. It helps to connect with a lightweight PLC or edge device that keeps data local yet accessible. When teams see the numbers, they push for small, repeatable improvements that compound over weeks and months, turning a good line into a standout asset for the plant floor.